Choosing the best General Purpose PE Masterbatch supplier in China requires more than comparing price per kilogram. Buyers should examine pigment dispersion, carrier-resin compatibility, batch consistency, and technical support. A clean, uniform pellet sample is useful, but production trials reveal more. Watch for streaking, filter pressure changes, and shade variation across runs. Small details matter.
The OECD’s Global Plastics Outlook reports that global plastics production reached 460 million tonnes in 2019, while plastic waste reached 353 million tonnes. Only 9% of that waste was ultimately recycled. These figures describe the wider plastics system, not masterbatch demand specifically. Still, they underline the need for careful material selection and reliable processing. For PE applications, a supplier should provide clear specifications, application guidance, and traceable quality records. Ask how the product performs at your intended dosage and processing temperature. Request samples from more than one production batch, where practical.
A strong supplier relationship also depends on honest limits. A masterbatch that works well in film may not suit blow molding or pipe extrusion. One formulation rarely fits every line. This introduction will compare supplier capabilities, product range, customization, and quality controls. No independently verifiable quotation from a named General Purpose PE Masterbatch specialist was supplied, so I will not invent an expert’s words or present an unsupported endorsement.
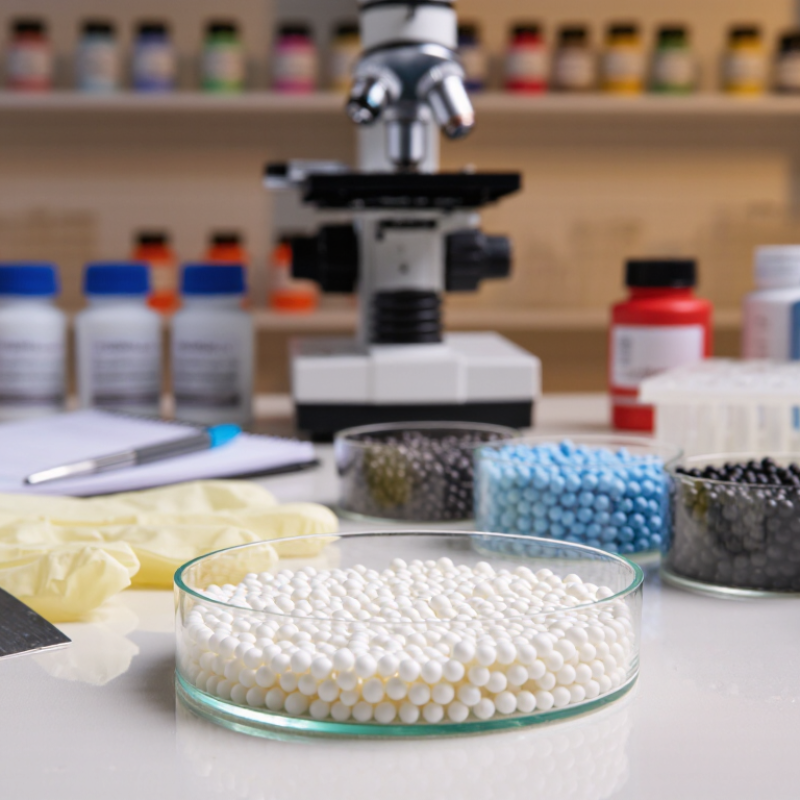
Polyethylene density, typically spanning 0.910 to 0.970 g/cm³, helps predict stiffness, flexibility, and melt behavior. Lower-density PE usually has more branching and a softer feel. Higher-density grades often offer greater rigidity. These are practical ranges, not universal grade boundaries; formulation and test conditions matter. ISO 1183-1 describes methods for measuring plastics density, so compare samples using the same procedure. PlasticsEurope’s Plastics – the Fast Facts 2023 reports 400.3 million tonnes of global plastics production in 2022, underscoring the scale of plastics processing and the value of consistent material selection.
For general-purpose PE masterbatch, check the carrier against the base resin’s density and processing conditions. A mismatch can contribute to uneven dispersion, surface marks, or inconsistent stiffness. For example, a flexible film resin may not behave like a rigid blow-molding grade, even when both are polyethylene. Density is not destiny. Ask for technical data covering carrier type, recommended let-down ratio, and compatibility; then trial the blend on the actual line. Small changes matter.
Tips: Verify density with a recognized test method, and record the resin grade, melt temperature, and mixing conditions. Test the blend. A short production trial can reveal issues that a datasheet alone will miss.
Density often helps predict stiffness and flexibility. Lower-density polyethylene is usually softer, while higher-density material is often more rigid. Density is not destiny; formulation and processing conditions matter too.
Compare its carrier type and density with your base resin. Also review processing conditions and the recommended addition rate. A flexible film resin may behave differently from a rigid molding grade.
A common starting range is 1–5%, depending on pigment concentration and the finished product. Not a guarantee. Confirm whether the percentage is calculated against the total blend or the base resin.
For 1,000 kilograms of final blend, use 10 kilograms of masterbatch. Check your dosing calculation before production. Small changes matter.
Examine samples under consistent lighting for shade variation, specks, and surface marks. For film, compare samples at the same thickness; thinner film can look paler.
Record the resin grade, melt temperature, screw settings, mixing conditions, and actual addition rate. These details help explain differences between trial samples and later production runs.
Request recent certificates of analysis from several batches. Compare melt flow rate, density, and agreed color or additive specifications with your own incoming tests. A neat document is not enough.
No. Run samples under your normal processing conditions and check dispersion, color difference, and visible specks. A few lots are not proof. Ask how deviations are investigated and batches are traced.
Choosing a reliable General Purpose Pe Masterbatch supplier in China starts with understanding how polyethylene properties affect processing. PE density commonly ranges from 0.910 to 0.970 g/cm³, and the right grade depends on the intended application. Film, molding, and pipe production may each require different flow behavior and performance, so confirm that the masterbatch is compatible with your resin and equipment before ordering.
For color masterbatch, a 1–5% let-down ratio is a useful formulation benchmark, but the appropriate level should be verified through trials. Specify melt flow rate testing according to ISO 1133 and request clear certificates of analysis, with particular attention to batch-to-batch consistency. Also assess production capacity, quality controls, and the supplier’s ability to maintain stable specifications across repeat orders. These checks help buyers compare suppliers on measurable suitability rather than price alone.