Top 10 PE Coloring Masterbatch Suppliers Worldwide

Time:2026-10-14 Author:Ethan
0%

Choosing the right Pe Coloring Masterbatch supplier requires more than comparing price lists. Polyethylene products serve packaging, agriculture, household goods, pipes, and industrial films. Each application demands controlled dispersion, stable shade, suitable carrier compatibility, and reliable processing performance. A masterbatch that looks excellent in a sample may behave differently during high-speed extrusion. That gap deserves attention.

Dr. Ramani Narayan, a polymer scientist and materials expert, has emphasized, “A formulation must be judged by performance, not appearance alone.” This principle guides our review of the Top 10 Pe Coloring Masterbatch Suppliers Worldwide. We examine pigment strength, color consistency, thermal stability, carrier selection, technical support, production capacity, and documented quality systems. We also consider whether suppliers can provide customized colors without weakening transparency, mechanical properties, or processing efficiency. Practical evidence matters. Factory experience matters more.

The ranking is not an absolute verdict. Regional availability, order volume, resin grade, and certification needs can change the best choice. Some suppliers offer impressive laboratories but limited flexibility for smaller buyers. Others provide competitive pricing, yet their technical documentation may feel incomplete. These differences are easy to overlook. They should not be.

A responsible purchasing decision should include trial batches, migration information where relevant, safety documentation, and performance testing under actual processing conditions. Buyers should also ask how suppliers manage pigment dispersion, shade tolerances, recycled polyethylene compatibility, and batch traceability. This guide aims to make that evaluation clearer. It may not answer every application-specific question, but it offers a grounded starting point for selecting a dependable Pe Coloring Masterbatch partner.
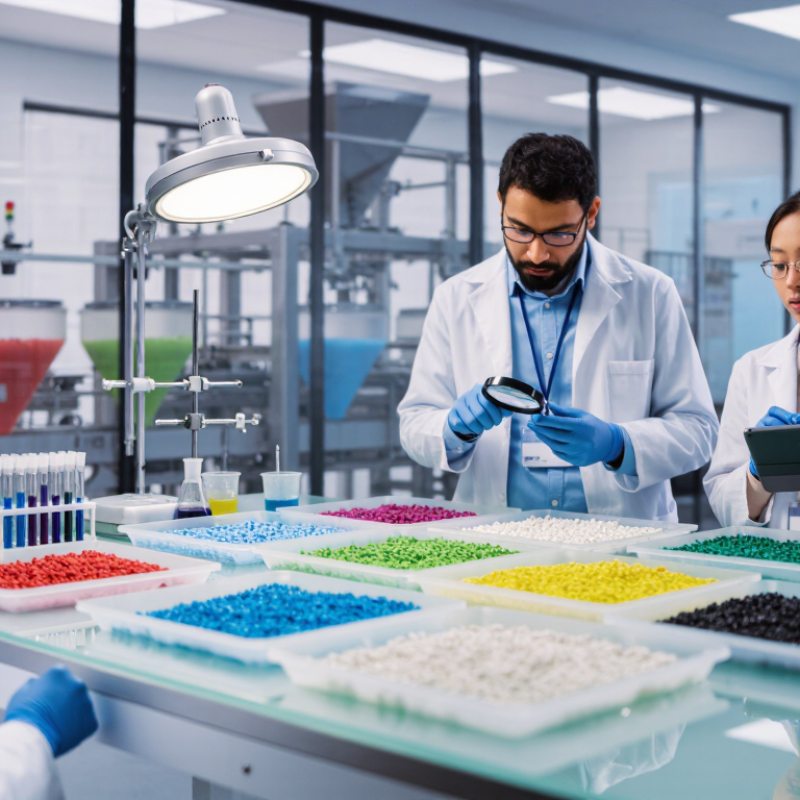
Top 10 PE Coloring Masterbatch Suppliers Worldwide

PE Coloring Masterbatch Basics: Carriers, Pigments, and 20–50% Loading

PE coloring masterbatch combines a polymer carrier with concentrated pigments and processing aids. The carrier should match the target resin, such as polyethylene used in film, pipe, or injection molding. Poor compatibility can create specks, weak weld lines, or uneven color. Small details matter.

20% to 50% Pigment loading commonly ranges from 20% to 50%, depending on shade strength and dispersion quality. Higher loading reduces dosing volume, but it can increase viscosity and agglomeration risk. Organic pigments often deliver bright shades, while inorganic pigments can provide stronger opacity and heat resistance. Carbon black needs careful dispersion, especially in thin film. A practical trial should check color difference, melt pressure, filtration residue, and tensile performance.

PlasticsEurope reported global plastics production of 413.8 million tonnes in 2023, showing the scale of resin demand behind masterbatch consumption. Market assessments from Smithers also identify packaging, construction, and consumer products as major application areas. However, published market figures vary because analysts define masterbatch differently. That limitation deserves attention. Supplier comparisons should therefore examine pigment loading, carrier chemistry, batch consistency, and technical support rather than headline capacity alone. In production trials, a 2% dosage may perform better than a cheaper 1% formulation, if dispersion remains stable.

Top 10 Global Supplier Profiles: Capacity, Regions, and Product Lines

Top 10 PE Coloring Masterbatch Suppliers Worldwide

A credible top-ten supplier review should compare capacity, regional reach, and product depth, not only color catalogs. PlasticsEurope reported global plastics production of 413.8 million tonnes in 2023. This scale keeps polyethylene masterbatch demand closely linked to packaging, agriculture, and consumer goods. Public supplier disclosures typically show annual masterbatch capacities from 10,000 to above 100,000 tonnes. However, capacity figures may include additives and non-PE products, so comparisons are imperfect.

The strongest global profiles usually combine plants in Asia, Europe, and the Americas. Regional producers often compete through shorter delivery times and customized shades. Product lines commonly include standard color concentrates, high-loading formulations, UV-stable grades, food-contact options, and recycled-PE-compatible systems. Packaging-focused suppliers may prioritize thin-film dispersion and low let-down ratios. Agricultural suppliers often emphasize weather resistance. Smithers identifies sustainability and recycled-content compatibility as major development themes in the plastics additives sector. Still, recycled polymers can create shade variation. That practical risk deserves more attention.

Tips: Request plant-level capacity, not group totals. Ask for COA samples, pigment migration data, and lot-to-lot color tolerance. Compare regional inventory, technical support, and minimum order quantities. A supplier with fewer colors may deliver better consistency. Test production-line performance before signing a long contract.

Top 10 PE Coloring Masterbatch Suppliers Worldwide - Top 10 Global Supplier Profiles: Capacity, Regions, and Product Lines

Rank Supplier Profile Estimated Annual Masterbatch Capacity Primary Operating Regions PE Coloring Specialization Typical Product Lines Processing Applications Technical and Sustainability Capabilities
1 Global Profile 01 More than 250,000 metric tons North America, Europe, Asia-Pacific, Latin America PE film colors White masterbatch Black masterbatch Custom colors Standard color concentrates, functional color systems, UV-stabilized colors, additive-color combinations Blown film, cast film, extrusion coating, injection molding, blow molding Global color matching, recycled-resin compatibility, food-contact grades, low-dosage concentrates
2 Global Profile 02 150,000–250,000 metric tons Europe, North America, Middle East, Asia-Pacific Polyolefin colors Black systems White systems Effect colors PE color concentrates, high-opacity white, carbon-black systems, pearlescent and metallic effects Packaging film, agricultural film, pipes, containers, caps and closures High-dispersion pigments, automated dosing support, weatherable grades, recycled-content formulation
3 Global Profile 03 100,000–150,000 metric tons Europe, Africa, Middle East, Asia-Pacific PE packaging colors Agricultural-film colors UV colors Film-grade concentrates, agricultural color systems, opaque colors, light-stable and weather-resistant grades Greenhouse film, mulch film, shopping bags, sacks, liners and flexible packaging UV and thermal stabilization, low-migration options, multilayer-film compatibility, batch consistency control
4 Global Profile 04 75,000–125,000 metric tons Europe, North America, Latin America, Asia-Pacific Custom PE colors High-opacity colors Special effects Custom color concentrates, opaque colors, translucent colors, fluorescent and visual-effect systems Injection molding, extrusion profiles, blow molding, film and rotational molding Laboratory color matching, small-batch development, pigment optimization, compliance documentation
5 Global Profile 05 50,000–100,000 metric tons North America, Europe, Asia-Pacific Film masterbatch White concentrates Black concentrates PE film colors, titanium-dioxide white, carbon-black concentrates, anti-block and slip combinations Stretch film, shrink film, agricultural film, lamination film and heavy-duty bags High pigment loading, film-gauge reduction support, recycled PE processing, food-packaging suitability
6 Global Profile 06 50,000–100,000 metric tons Europe, Middle East, Africa, Asia-Pacific Polyethylene pipes Cable compounds Industrial colors Pipe-grade black, blue and brown systems, signal colors, long-term UV-resistant concentrates Pressure pipes, gas pipes, cable jacketing, conduit, tanks and industrial molded parts Long-term heat and weather resistance, carbon-black dispersion control, pressure-pipe compliance support
7 Global Profile 07 25,000–75,000 metric tons North America, Europe, Latin America Specialty color concentrates Consumer packaging colors Fluorescent colors Custom PE colors, neon and fluorescent systems, transparent colors, premium appearance concentrates Personal-care packaging, household containers, caps, closures, toys and consumer products Rapid color development, appearance control, small production runs, pigment and resin compatibility testing
8 Global Profile 08 25,000–75,000 metric tons Europe, United Kingdom, Middle East, Asia-Pacific PE film colors Recycled-PE colors Sustainable formulations Color concentrates for flexible packaging, recycled-polymer grades, low-carbon formulations and mono-material systems Flexible packaging, courier bags, refuse sacks, liners, agricultural film and consumer film products Recycled-resin tolerance, odor and contamination management, reduced-carbon product options, mono-material design support
9 Global Profile 09 15,000–50,000 metric tons Asia-Pacific, Europe, Middle East, Africa Cost-efficient PE colors White masterbatch Black masterbatch General-purpose colors, high-concentration white, black concentrates, packaging and agricultural grades Film extrusion, woven sacks, raffia, injection molding, household products and agricultural applications Competitive high-volume production, standard color libraries, export packaging, routine quality-control testing
10 Global Profile 10 10,000–40,000 metric tons Asia-Pacific, Europe, North America, Latin America Niche PE colors Biodegradable-polymer colors Custom low-volume colors Specialty color concentrates, biodegradable-polymer-compatible colors, additive-color packages and private formulations Flexible packaging, agricultural products, consumer goods, 3D-printing filament and specialty extrusion Flexible minimum order quantities, application trials, biodegradable-resin compatibility, custom formulation services

Capacity figures are presented as industry-estimate ranges for masterbatch production and are intended for supplier screening. Actual capacity varies by facility, product mix, utilization rate and reporting period. Product availability and regulatory suitability should be confirmed directly with each supplier.

Supplier Selection Criteria: Capacity, ISO 9001, and Global Distribution

For a Top 10 PE coloring masterbatch list, production capacity deserves careful checking. Plastics Europe reported global plastics production of 413.8 million tonnes in 2023. This scale creates strong demand for stable, high-volume color supply. However, a large nameplate capacity can mislead. Buyers should request monthly output, reactor or compounding-line details, lead times, and recent shipment records. Ask whether capacity remains available during peak seasons.

ISO 9001 ISO 9001 is a useful quality baseline, not automatic proof of color consistency. The ISO Survey 2023 recorded more than 1.2 million ISO 9001 certificates worldwide. A serious supplier should provide a current certificate, site address, certification scope, and audit status. Check whether the certificate covers masterbatch production. Request batch-to-batch ΔE data, pigment dispersion results, and retain-sample procedures. Small details matter.

Global distribution Global distribution requires more than a warehouse map. The World Bank’s Logistics Performance Index 2023 showed clear differences in customs efficiency, infrastructure, and shipment reliability between markets. Evaluate regional inventory, export documentation, packaging protection, and technical response times. Ask for delivery performance across your target countries. One weakness remains easy to overlook: some suppliers promise worldwide service but depend on a single export hub. A trial order can reveal the truth.

Technical Benchmarking: ΔE00, Dispersion, and MFR Under ISO 1133

Top 10 PE Coloring Masterbatch Suppliers Worldwide

Technical Benchmarking: ΔE00, Dispersion, and MFR Under ISO 1133

A serious comparison of PE coloring masterbatch suppliers starts with test control, not catalog claims. ΔE00 values should come from identical plaques, lighting conditions, and instrument settings. A difference below 1.0 may appear invisible, yet the result depends on gloss, surface texture, and the chosen color standard. Record the illuminant, observer angle, and batch number. Small details matter.

Dispersion testing reveals whether pigment particles distribute evenly through polyethylene. Microscopy can expose agglomerates that remain hidden during a quick visual check. Pressure-filter testing adds practical evidence, especially for film and extrusion applications. During production trials, watch for streaks near the die lip and color variation across the roll. Perfect dispersion on paper can still fail at higher output.

MFR testing under ISO 1133 requires the same temperature, load, die, and conditioning procedure. A masterbatch may shift the compound’s flow rate, even when the carrier appears compatible. Compare the neat PE, let-down blend, and final colored formulation. A stable MFR supports predictable feeding and extrusion. But it does not guarantee good processing.

Real benchmarking is rarely clean. Operators, moisture, and pigment loading can distort results. Repeat each test across several batches. Report the variation, not only the best value. That makes supplier data more useful, although some uncertainty will remain.

Technical Benchmarking of PE Coloring Masterbatch Suppliers

The chart compares ten anonymized benchmark samples using CIEDE2000 color difference (ΔE00), optical dispersion score, and melt mass-flow rate (MFR) measured under ISO 1133. Lower ΔE00 indicates closer color matching, higher dispersion scores indicate more uniform pigment distribution, and MFR values are shown in g/10 min. Results are representative benchmark values; actual performance depends on resin grade, pigment loading, processing temperature, and test conditions.

Application and Compliance: PE Films, Pipes, REACH, RoHS, and FDA Rules

For a Top 10 PE Coloring Masterbatch Suppliers Worldwide review, application fit matters more than catalog size. PE films require strong dispersion, low plate-out, and stable shade at thin gauges. Pipes need weathering resistance, pressure durability, and controlled pigment loading. PlasticsEurope reported 413.8 million tonnes of global plastics production in 2023, showing the scale of demand for consistent polymer additives.

Compliance must match the final article, not only the masterbatch. Under EU REACH, suppliers should disclose substances of very high concern and provide updated safety documentation. RoHS limits ten restricted substances, including lead, mercury, and certain phthalates, but it mainly targets electrical and electronic equipment. It does not automatically govern every PE film or pipe. That distinction is often overlooked.

For food-contact films, manufacturers should verify the colorant and carrier against applicable FDA requirements, including 21 CFR 177.1520 for olefin polymers. Migration testing, batch traceability, and a current certificate of analysis provide stronger evidence than a generic compliance letter. I would also request SDS records, technical data, and independent test results. A certificate is not proof for every formulation. Processing temperature, recycled content, and pigment concentration can change performance. Supplier comparisons should record these variables, although many published rankings do not.

FAQS

What makes a fair comparison of PE coloring masterbatch suppliers?

Use identical plaques, lighting, instruments, color standards, and batch records. Record the illuminant and observer angle. Small settings matter. Catalog claims are not enough.

What does ΔE00 reveal?

It measures color difference between a sample and a reference. Below 1.0 may look invisible. Gloss and surface texture can change perception. Never treat one value as universal.

How should pigment dispersion be tested?

Combine microscopy with pressure-filter testing. Microscopy can reveal hidden agglomerates. Pressure filters reflect extrusion conditions. Watch the die lip for streaks. Paper results can disappoint.

Why should film and pipe applications be tested differently?

Thin PE films need strong dispersion, low plate-out, and stable shade. Pipes need weathering resistance and pressure durability. One formulation may not suit both. Application fit beats a large catalog.

How is MFR tested under ISO 1133?

Keep temperature, load, die, and conditioning identical. Test neat PE, the let-down blend, and final colored compound. Stable MFR supports predictable feeding. It still cannot guarantee smooth processing.

Which production variables can distort benchmark results?

Operators, moisture, pigment loading, and output rate can change results. Repeat tests across several batches. Report variation, not only the best result. Uncertainty remains. That is normal, though inconvenient.

What compliance documents should buyers request?

Request SDS records, technical data, current certificates of analysis, and independent test results. Check substance disclosures under REACH. Verify restricted substances under RoHS when electrical equipment applies. A generic letter is weak evidence.

What should food-contact PE film manufacturers verify?

Confirm the colorant and carrier meet applicable food-contact requirements. Check relevant FDA rules, migration data, and batch traceability. Review the final formulation, not just the masterbatch. Recycled content and pigment concentration may alter results. I would verify twice.

Conclusion

This article provides a practical overview of Pe Coloring Masterbatch, explaining how carrier resins, pigments, additives, and typical 20–50% pigment loading influence color strength, processing stability, and final product performance. It introduces the key factors used to compare global suppliers, including production capacity, regional coverage, ISO 9001 quality systems, technical support, and distribution capabilities. The discussion also highlights how product lines may be matched to different polyethylene grades and manufacturing requirements.

For technical evaluation, the article focuses on color consistency measured by ΔE00, pigment dispersion, and melt flow rate tested under ISO 1133. It further examines suitability for PE films, pipes, packaging, and other applications, while emphasizing the importance of REACH, RoHS, FDA, and relevant regional compliance requirements. By combining supplier assessment with laboratory benchmarking and application-specific testing, buyers can select reliable materials that deliver consistent appearance, efficient processing, and dependable regulatory performance.
Ethan

Ethan

Ethan is a seasoned marketing professional with a deep expertise in our company's innovative product line. With a passion for sharing knowledge and insights, he takes the lead in regularly updating our corporate blog, where he explores industry trends, product features, and effective marketing......