Engineered for high color yield, thermal stabilization up to 260°C, and structural polymer compatibility across blown film, blow molding, and pipe extrusion lines.
Strategic analysis of local manufacturing infrastructure, Caribbean climatic stressors, and commercial material requirements.
Situated within Saint Paul Parish, Liberta serves as a central hub connecting agricultural valleys with southern logistical centers. The micro-industrial sector relies heavily on converting imported raw polyethylene (LDPE, LLDPE, HDPE) into utilitarian goods, packaging liners, potable water conduits, and architectural profiles. Sourcing reliable pigment systems locally is a recurring challenge, demanding supply partnerships that eliminate batch variances and inventory downtime.
Liberta's geographic location exposes finished plastic parts to sustained UV indices exceeding 11, high ambient humidity (averaging 78%), and airborne chloride aerosols. Standard unformulated pigments undergo fast photo-oxidation, leading to embrittlement, matrix chalking, and catastrophic color fading. Polymers deployed in Liberta require Rutile-grade titanium dioxide (TiO₂), synergistic hindered amine light stabilizers (HALS), and carbon black with sub-25nm primary particle sizes.
Regional development across Antigua drives strong demand for robust, non-migrating plastic articles. From underground civil utility piping to drip-irrigation piping in agricultural nurseries, processors in Liberta demand additive and colorant packages that withstand elevated extrusion backpressures, high screw shear rates, and varying ambient shop-floor temperatures without dielectric breakdown.
Bridging polymer physics with localized application scenarios across agricultural, infrastructural, and packaging operations.
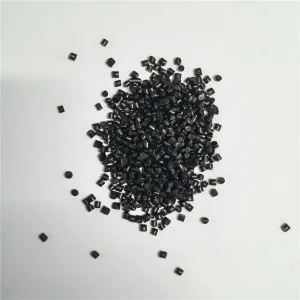
Local cultivation around Liberta requires advanced blown film mulches. Our high-dispersion Carbon Black masterbatch provides total solar opacity to eliminate weed germination beneath beds, while specialized PE White grades reflect excessive infrared radiation, cooling underlying root temperatures. Tight pigment dispersion ensures zero pinholing even at film gauges under 15 microns.
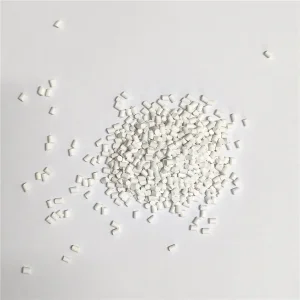
With regional logistics expanding, blown co-extrusion films require dual-layer differentiation: opaque white exterior skins for high-contrast barcode printing and solid jet-black interior layers for complete package confidentiality. Formulated with linear low-density polyethylene (LLDPE) carriers, our compounds retain dart-impact strength and heat-seal integrity along side seams.
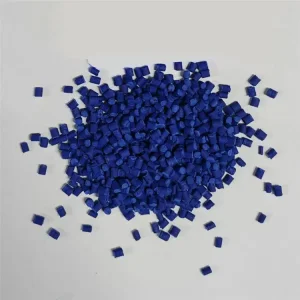
Civil infrastructure throughout the Leeward Islands requires PE100 pipe extrusion with certified long-term thermal stability. Our blue PE masterbatch meets strict food-contact criteria for municipal water transport, incorporating micro-milled organic pigments that do not nucleate prematurely or cause longitudinal stress cracks under fluctuating cyclic hydrostatic pressures.
Engineering Recommendation for Liberta Extruders: Due to localized ambient humidity fluctuations, we suggest running pre-extrusion moisture assays. Our products undergo vacuum degassing during extrusion, ensuring an ambient moisture content below 0.15% to stop surface splay, lens creation, or melt fracture at the die lip.
Leveraging high-precision twin-screw compounding lines, direct raw material integration, and rigorous QC to support island manufacturing economies.
Operating a modernized 6,000 m² facility with co-rotating, high-torque twin-screw extruders allows superior shear-rate control. Pigment aggregates are broken down below 2–5 microns, thoroughly coated with specialized processing waxes, and locked into the carrier matrix. This eliminates specking, screen blockage, and uneven melt viscosity on clients' factory floors.
Located in Changzhou, Jiangsu, Jiazhou sits at the heart of the Yangtze River Delta chemical corridor. Direct contracts with primary TiO₂, carbon black, and virgin polyolefin suppliers insulate partner convertors in Liberta from global spot-market swings, shipping bottlenecks, and resin shortages, maintaining stable unit economics.
Our R&D division is actively rolling out universal and post-consumer recycled (PCR) compatible masterbatches. Engineered to lower the carbon footprint of island economies, these systems improve compatibilization across mixed-waste polyolefin streams while delivering deep, uniform coloration at low let-down ratios (1% to 4%).
| Masterbatch Grade | Carrier Resin | Active Pigment / Additive Loading | Thermal Stability | Melt Flow Index (190°C/2.16kg) | Primary Target Applications |
|---|---|---|---|---|---|
| JZ-BLU-902 | LLDPE / LDPE | 35% Phthalocyanine Blue | 260°C | 12 - 18 g/10min | Potable Pipes, Drums, Blown Film |
| JZ-WHT-101 | Virgin LDPE | 60% Rutile Titanium Dioxide | 280°C | 8 - 14 g/10min | Courier Film, Dairy Bottles, Sheet |
| JZ-BLK-800 | LLDPE Universal | 40% High-Jet Carbon Black | 260°C | 10 - 15 g/10min | Agri-Mulch, Geomembranes, Conduit |
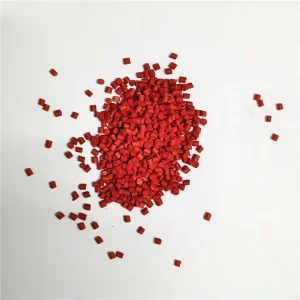
| JZ-RED-404 | Homo-PP / PE | 30% Azo Condensation Red | 240°C | 15 - 22 g/10min | Caps, Crates, Consumer Injection |
| JZ-MET-GLD | Low-Melt PE | 25% Metal-Alloy Flake / Pearl | 220°C | 18 - 25 g/10min | Cosmetics, Luxury Blow Molded Vessels |
Ensuring cross-border compliance, zero material degradation during transit, and precise on-site color formulation.
Every masterbatch batch leaves our facilities compliant with REACH, RoHS, FDA 21 CFR food-contact standards, and EN71-3 toy safety parameters. We supply exhaustive Certificates of Analysis (COA), safety data sheets (SDS), and migration assay reports with every consignment, eliminating regional customs clearance hurdles across Antigua and Barbuda.
To withstand trans-oceanic shipping to Saint John’s port and subsequent warehousing in Liberta, our products are sealed in 25kg multi-layer Kraft-aluminum composite moisture-barrier bags, shrink-wrapped, and fully palletized. This prevents moisture uptake during humid sea voyages, ensuring dry resins enter clients' feed throats directly from the bag.
Operating a modern color laboratory with advanced spectrophotometers, our technicians match custom PANTONE, RAL, or physical resin swatches within 3 to 5 working days. Sample batches of 1kg to 5kg are air-freighted directly to testing centers in Liberta for immediate trial runs and extruder calibration.
Addressing core manufacturing challenges, shipping logistics, and additive selection for plastics converters in Liberta.
Our high-concentration masterbatches typically achieve saturated, opaque coloration at let-down ratios between 1.5% and 3.0%. For thin agricultural films (<25 microns), an LDR of 2.0% to 4.0% is recommended to ensure uniform light-barrier performance and mechanical integrity.
We blend our exterior-grade colorants with concentrated Rutile Titanium Dioxide (minimum 94% purity) and Hindered Amine Light Stabilizers (HALS). These additives capture free radicals induced by intense Caribbean UV radiation, preventing surface micro-fissures and chalking.
Standard orders are processed, compounded, and dispatched from our factory within 10 to 15 business days. Cargo moves via ocean freight from Ningbo or Shanghai port straight to Saint John's Port, Antigua, where regional forwarders handle transport directly to Liberta facilities.
Yes. While LDPE/LLDPE carriers cover broad applications, we formulate grades using PP, HDPE, EVA, or universal carrier systems. This maintains melt index parity between the masterbatch and primary base resins, preventing delamination or die drool.
Advanced, non-migrating, heat-resistant formulations for blow-molded bottles, industrial sheets, and performance profile extrusions.